

Bucket Elevators
PPM Technologies bucket elevators are designed to elevate a wide range of dry, free-flowing products, including nuts, snack foods, cereals, pet foods, confectionary products and more.

Raw Receiving Conveyor
The CMP line of raw receiving conveyor solutions couples rugged heavy-duty construction with ease of sanitation features.

Vibraflex ii
PFI VFII sanitary vibratory conveyor efficiently and seamlessly moves a variety of products throughout your food processing line. Its flexible for multiple value-added applications, such as screening, shaking, laning, grading, and spreading.

Hex Spreader
The FoodeQ Hex Spreader can be applied to grade and clear potatoes and other root vegetables from debris and sand. Also, the machine can spread a small product flow over the full width of the machine in a very short distance.

Libra Mass Flow
PPM’s Libra VF Mass Flow System employs a two-tier conveyor system that combines VF technology with load-cell scales, measuring product by both weight and volume.

Even Flow Bins
CMP Manufactures several styles of even flow bins to provide surge capacity in raw receiving applications as well as other process and packaging areas.
Sponsored Content
Sponsored Content
Sponsored Content

SB 651 Receiving hopper of 12-14 m³
De SB 651 is een efficiënte stortbunker met een bunkerinhoud van 12-14 m³ en een 2 meter brede productvriendelijke bunkervloer. Diverse units kunnen achter de bunker geplaatst worden.

Mini VF Electromagnetic Vibratory Motion Conveyor
The PPM Technologies Mini VF is a small yet powerful electromagnetic vibratory motion conveyor that boasts a variety of versatile mounting options, adjustable feed rates, an open and sanitary design, low maintenance costs, and a long and dependable life cycle.

Dosing Vibratory Conveyors
Vibratory Conveyor to dose product on a belt by varying the stroke step from 0-9 mm.

Hopper Feeder
PFI Hopper Feeder allows processors to more efficiently load, store, and feed product throughout food processing lines.
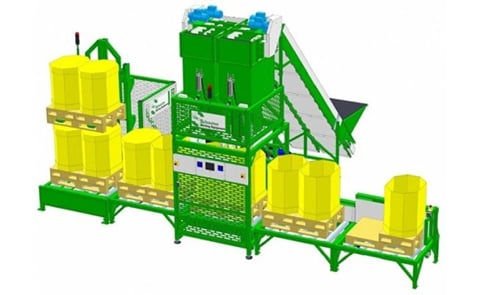
Octabin Filler
Complete system to automatically weigh, fill and stack octabins (boxes of 200 kg). Capacity of 30 pallets per hour, 2 minutes per pallet.

Self-cleaning and disinfecting screw conveyor
The automatically controlled process leads to complete control of water and chemical consumption. The automatically controlled process leads to complete control of water and chemical consumption.
Sponsored Content

Accumulation Trays
Optimize product flow regulations and homogenize the flow rate, using accumulation hoppers as required.
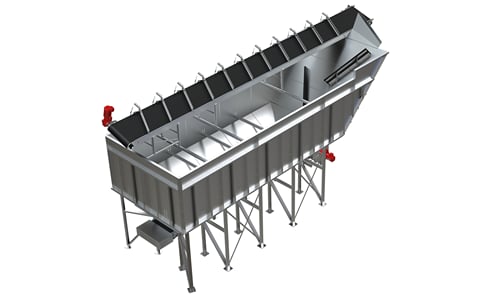
Even Flow Bins
Southern Fabrication Works offers a range of even flow bins with a wide range of capacities an with multiple filling and discharge options, designed to create a smooth and consistent product flow

SB 151 Receiving hopper of 5–6 m³
De SB 151 is de kleinste stortbunker (5-6 m3 bunkerinhoud) uit het Dewulf-gamma, maar de machine is wel uitgerust met de belangrijkste kenmerken, zoals productvriendelijkheid. Deze stortbunker is de keuze van telers met een beperkt areaal.

Bucket-Elevator
PFI Bucket Elevator conveyor elevates your product to the next step in your food processing line in a tight footprint.

Inclined or Vertical Elevators
Tecno Alimentaria Valenciana (TAV) have two models: standard and with external chassis. The external chassis allows the interior cleaning, it is accessible to have control points, and in this way to control that there are no product remains inside.

Purlift
Purlift positive drive vertical lift conveyor fits in tight spaces where you need to elevate your food processing line. Its positive drive system and self-tracking belt keep your product and operation moving.