

Retractor
PFI Retractor retracting belt conveyor adds flexibility to the fixed space of your food processing plant. It performs several applications in one machine – from loading and depositing to transferring, rejecting, and positioning.

Eqlipse dosing vibratory conveyor
The FoodeQ Eqlipse is designed to turn bulk into batches with a high accuracy. The Eqlipse features a dosing vibratory conveyor in combination with a single head weigher.
Magneflex
PFI Magneflex sanitary vibratory conveyor efficiently and seamlessly moves a variety of products throughout your food processing line. Its flexible for multiple applications, such as feeding, spreading, and laning.

Vibratory Shaker
The CMP line of vibratory shakers have been designed to convey, sort, or size food products of all shapes and sizes.
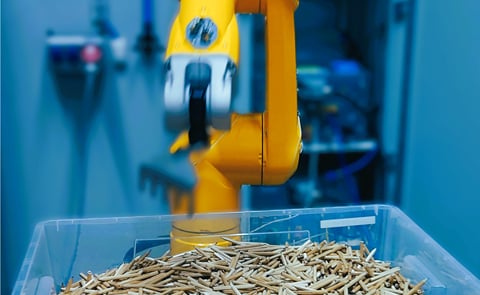
Volumax
The Volumax is a system designed to optimize the filling of bulk and piece goods. This system provides a solution to more efficiently fill containers with loose products, such as frozen products.
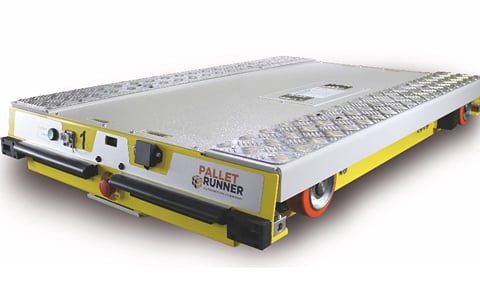
Pallet Runner- Semi-Automated
By combining Semi-Automated Pallet Runner Carts with either conventional Forklifts or AGV’s, maximize density in your freezer beyond what is possible with Drive-In or Push Back Systems. Reduce your rack, product, and truck damage and increase your productivity with proven technology.
Sponsored Content
Sponsored Content
Sponsored Content

Accumulation Trays
Optimize product flow regulations and homogenize the flow rate, using accumulation hoppers as required.

Dewatering Shaker
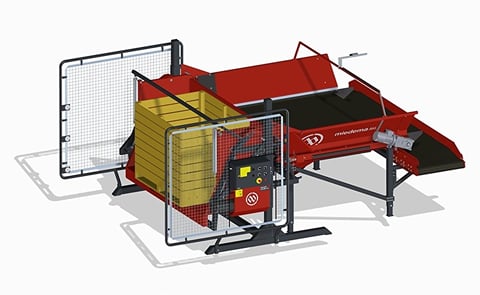
FoodeQ designs and builds professional shakers exactly according to our customers’ requirements and wishes for a wide range of products and purposes.

Vibratory Length Graders
FoodeQ has experience in grading/sorting a wide range of products, including french fries.

H-Flow Conveyor
FoodeQ designs and builds H-Flow conveyors exactly according to their customers’ requirements and wishes, for the gentle horizontal handling and conveying of delicate food products.

SB 151 Receiving hopper of 5–6 m³
The SB 151 is the smallest receiving hopper (5–6 m3 bunker capacity) from the Dewulf product range. However, the machine is equipped with the necessary features. This receiving hopper is the right choice for smaller growers.
Sponsored Content
EDF Feeder
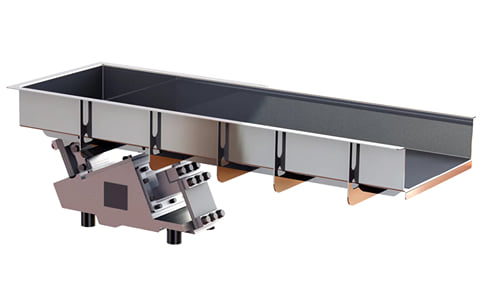
PFI EDF Feeder sanitary vibratory feeder efficiently moves a variety of products throughout your food processing line.

Sanitary Conveyor–mesh Metal Belt
CMP routinely works with leading metal belt manufacturers including Marcon and Cambridge to deliver best in class sanitary conveyor solutions.

PMC
As the industry demands larger product capacity, greater product variability, and longer conveying distances, SV Agri continually strives to develop innovative PMC systems.
SB 451 Receiving hopper of 10-12 m³
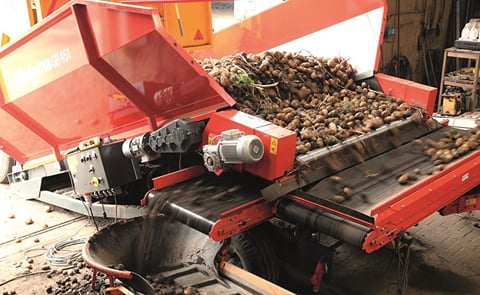
The SB 451 is a small receiving hopper with large capacities and has a bunker capacity of 10-12 m³. This product-friendly receiving hopper can be equipped with a combination of various options both in the field of cleaning and sorting.

Horizontal Belt Conveyor
PFI Horizontal Belt Conveyors are common conveying solutions to move product throughout your food processing plant.
