
Defoaming Agents in the Potato Processing Industry
Defoaming agents are specialized process aids used throughout the potato processing industry to control unwanted foam. During washing, peeling, cutting, starch extraction and other processing operations, potatoes release starch, soluble proteins and other surface-active compounds into process water. Mechanical agitation, pumping, turbulence and air entrainment can then cause foam to form and persist in processing systems.
Uncontrolled foam can lead to tank overflow, reduced processing capacity, pumping difficulties, poor separation efficiency, inaccurate level monitoring, production interruptions and increased water and cleaning requirements. Defoaming agents help control these problems by breaking down existing foam and reducing further foam formation. Depending on the application, they are used in potato washing systems, French fry and potato chip processing, potato starch production, potato protein recovery and wastewater treatment. In food-processing applications, the selected defoamer must also comply with applicable food-contact, safety and regulatory requirements in the target market.
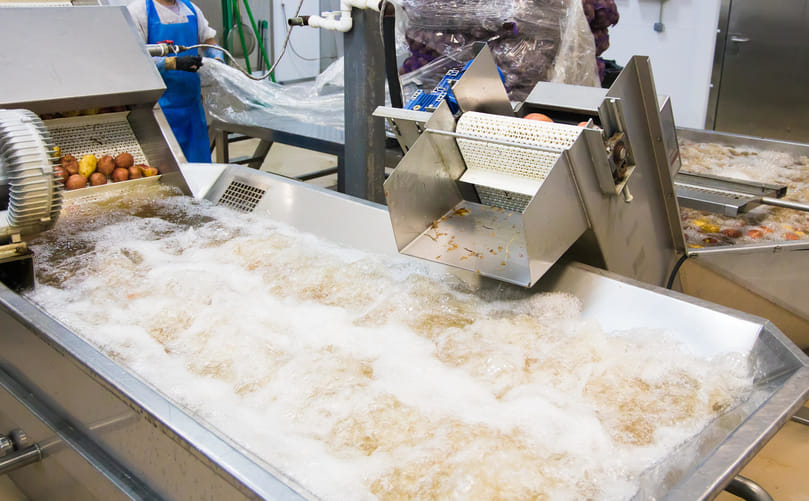
Industrial Defoamers for Potato Processing
What Are Defoaming Agents?
Defoaming agents, also known as defoamers or antifoams are substances added to process liquids to control, reduce or eliminate unwanted foam. In technical usage, an antifoam is primarily intended to prevent foam formation, while a defoamer is generally used to break down foam that has already formed. Both work by destabilizing the thin liquid films (lamellae) surrounding air bubbles, causing the bubbles to collapse.
In commercial practice, however, the terms defoamer and antifoam are often used interchangeably. Many products used in potato processing provide both rapid knockdown, which collapses existing foam and hold down, which helps prevent foam from reforming. These products may be formulated as emulsions, dispersions or concentrated compounds based on silicone, mineral or vegetable oils, polyether or other materials. Their selection depends on factors such as processing conditions, temperature, pH, food contact requirements and the specific stage of potato processing.
Why Does Foam Form During Potato Processing?
Foam formation during potato processing results from the combination of foam active potato components in process water and mechanical incorporation of air. When potatoes are washed, peeled, cut, sliced or transported through water, cellular material is released into the process stream. The resulting water can contain starch, soluble proteins, fibers, sugars and other organic compounds. As these materials accumulate in process water, they can contribute to foam formation and persistence.
Potato Components That Promote Foaming
Fresh potatoes typically contain about 75–80% water with the remaining fraction consisting mainly of carbohydrates, including starch along with protein, fiber, minerals and other compounds. The exact composition varies with cultivar and growing conditions.
Potato proteins are particularly important for foam formation and stabilization. Major potato proteins include patatin and protease inhibitors, which have surface active properties and can accumulate at the air water interface. This helps form and stabilize the films surrounding air bubbles, allowing foam to persist.
Starch is another important contributor in industrial potato processing. Washing, peeling and cutting can release starch into process water, increasing the concentration of suspended solids and under suitable conditions, the viscosity of the liquid. Higher viscosity can slow drainage from foam films and contribute to foam persistence. Therefore, it is more accurate to describe potato proteins as important foam active substances, while starch acts as an important foam promoting and foam stabilizing component, rather than classifying both simply as surfactants.
Processing Conditions That Increase Foam
Several processing operations can increase foam because they continuously introduce air into water containing starch, proteins and other potato-derived materials:
- Continuous water circulation and recirculation in flumes, wash tanks and process water systems
- High shear pumping, agitation and turbulence
- Mechanical peeling, cutting and slicing
- Washing and rinsing that remove surface and cellular starch
- Hydro transport and other operations that promote air entrainment
- Increasing concentrations of starch and soluble organic material in recirculated process water
Temperature can also influence foaming, but its effect is more complex. Changes in temperature can affect protein structure, liquid viscosity and other interfacial properties, thereby altering foam formation and stability. However, heating does not necessarily increase foam; sufficiently high temperatures can denature and precipitate potato proteins, changing their ability to stabilize foam.
Overall, persistent foam in potato processing is best understood as the result of foam active potato proteins, starch and other solids accumulating in process water, combined with continuous mechanical incorporation of air. The severity of foaming depends on potato composition, the amount of material released into the water, solids concentration, water recirculation, turbulence, equipment design and operating conditions. Foam can therefore become a recurring operational issue in potato washing, peeling, slicing and other water-based processing systems.
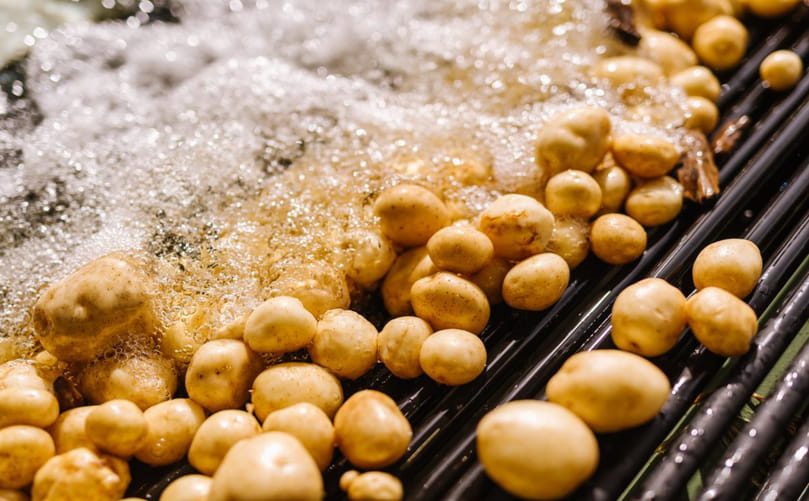
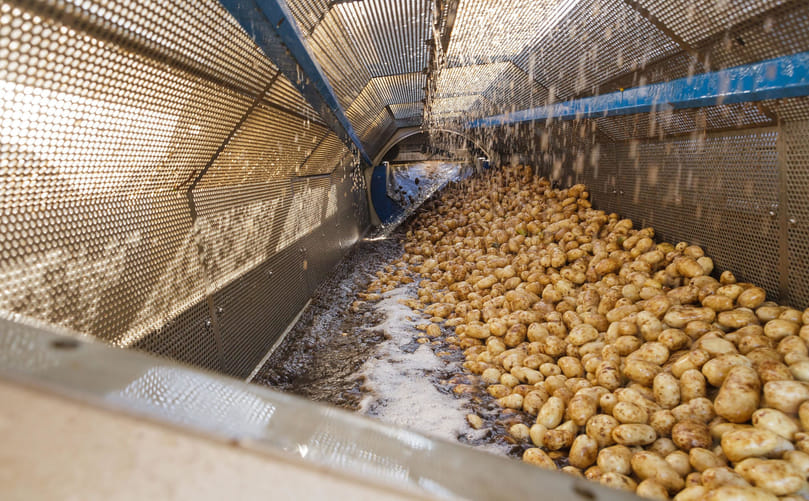
Foam Formation in Potato Processing Water
Where Are Defoaming Agents Used in the Potato Industry?
Defoamers and antifoams are used in selected water intensive and foam prone operations in the potato processing industry. Their use depends on the process design, the amount of starch and protein entering the water, mechanical air entrainment, temperature, wastewater characteristics and applicable food safety requirements. They are particularly relevant where foam can interfere with equipment operation, process control, product handling or wastewater treatment.
Potato washing — Washing tanks, drum washers, flumes and recirculated process water systems can generate foam as soil, starch, proteins and other organic material enter the water. Excessive foam can interfere with water circulation, sensors, equipment operation and process water management.
Peeling and cutting — Abrasive, steam and mechanical peeling, followed by cutting or slicing can release starch and other cellular components into water systems. Turbulence, pumping and air entrainment can then promote foam formation in transport and rinse water.
Blanching — Blanching involves hot water, commonly at approximately 70–90 °C depending on the product and process. Foam can develop when organic material and air are present in blanching systems. Where an antifoam is required, the formulation must be suitable for the operating temperature and the intended food processing application.
French-fry processing — Foam control may be required in washing, rinsing, starch removal flumes and recirculated process water systems. Controlling excessive foam can help maintain stable water circulation and reduce foam carry over between process stages.
Potato-chip processing — Washing and slicing operations can release free starch into process water, while recirculation and turbulence can promote foaming. Where foam becomes operationally significant, antifoam treatment may be considered in washing or starch management systems.
Potato starch production — Foam can occur during potato washing, rasping or grinding, starch pulp separation, potato juice handling and other liquid-processing stages. Rasping disrupts potato cells and releases starch and potato juice, while subsequent separation and pumping can introduce air. Foam control may therefore be required at specific points depending on plant design and process conditions.
Potato protein processing — Protein rich potato juice and related liquid streams can be particularly foam prone because potato proteins have surface active properties. Foam may occur during juice concentration, heating, coagulation and separation, making foam control an important consideration in some potato protein recovery processes.
Potato-processing wastewater — Foam can occur in collection and equalization tanks and during biological wastewater treatment, particularly where high organic loading, surfactants and aeration introduce or stabilize air bubbles. Defoamers may be used when excessive foam interferes with treatment operation or equipment.
The use of a defoamer is not automatically required at every processing stage. Many plants control foam through equipment design, process water management, filtration, reduced air entrainment or other operational measures before considering chemical treatment. Where a defoamer or antifoam is used in a food-processing environment, the product must be appropriate for the specific application and comply with the relevant regulatory and customer requirements.
Selection and dosing depend on factors such as temperature, pH, starch and protein concentration, water chemistry, mechanical agitation, residence time and the location of foam formation. Food-contact applications require particular attention to the applicable regulations and the manufacturer's permitted use level. In wastewater treatment, the selection must also consider potential effects on biological treatment and downstream operations.
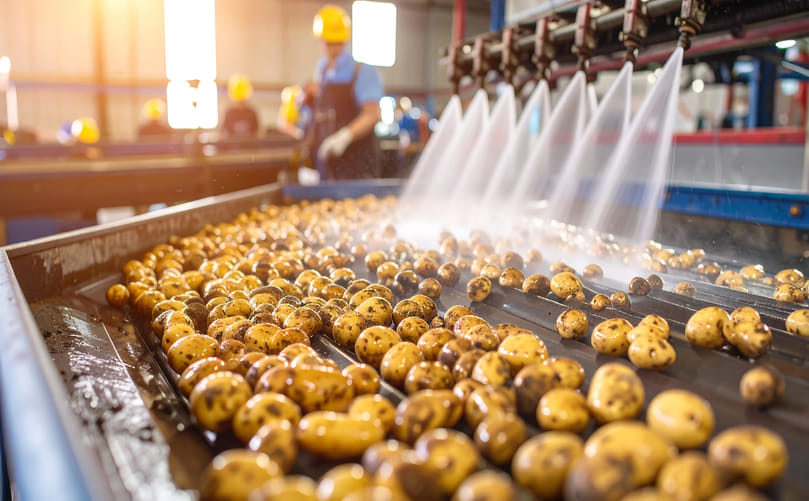
Where Are Defoaming Agents Used in the Potato Industry?
Types of Defoaming Agents Used in Potato Processing
Potato processors select defoamers according to the process conditions, including temperature, starch and protein load, water chemistry, foam severity, food contact requirements and regulatory restrictions. The main types include:
Silicone-based defoamers: Silicone-based defoamers commonly contain polydimethylsiloxane (PDMS), either as an emulsion or in combination with other carrier materials. They have very low surface tension, provide rapid foam knockdown and can remain effective over a relatively wide temperature range. They may be used in water intensive processing systems where persistent foam develops, although the suitability of a particular grade depends on its food contact authorization and the applicable regulations. Their effectiveness at relatively low use levels makes them attractive for difficult foam control applications.
Oil-based defoamers: Oil-based defoamers use carriers such as vegetable oils or certain mineral oils and may contain hydrophobic solids or other active ingredients that destabilize foam. They can be suitable for washing, conveying and other aqueous processing systems where silicone free foam control is preferred. However, not all oil-based defoamers are suitable for direct food contact, so the specific formulation and regulatory status must be checked before use.
Water-based defoamers: Water-based defoamers are formulations in which oil, wax, silicone or other foam control ingredients are dispersed in water. They are easy to disperse into aqueous process streams and can be suitable for continuous dosing. Their performance depends strongly on the active chemistry and formulation making them useful for applications such as potato washing, rinsing and other water-intensive processing operations.
Polyether and EO-PO defoamers: Polyether-based defoamers, including some ethylene oxide-propylene oxide (EO-PO) copolymers are designed for applications requiring good foam control and compatibility with aqueous systems. Some grades provide effective performance at elevated temperatures and can also offer useful deaeration properties. They may be selected for specific process conditions where silicone-based products are unsuitable or where a silicone free formulation is preferred. Food-contact suitability must be established for the individual product rather than assumed from its chemical class.
Bio-based and vegetable-oil-based defoamers: Bio-based defoamers can contain vegetable oils, fatty-acid derivatives, fatty alcohols, esters or other renewable feedstocks. They are increasingly considered where processors want to reduce dependence on petroleum derived ingredients or meet specific sustainability requirements. However, bio-based does not automatically mean food grade, clean label, biodegradable or organically certified. These properties depend on the complete formulation and the certification or regulatory status of the individual product.
Commercial defoamers are often formulated as blends of several components rather than relying on a single active ingredient. In potato processing, performance can be affected by starch, proteins, dissolved solids, detergents, temperature, water hardness and mechanical air entrainment. Therefore, processors normally select a product based on the specific process stage, applicable food contact regulations, supplier specifications and plant trials.
How Do Defoaming Agents Work?
Foam consists of air bubbles surrounded by thin liquid films, known as lamellae. In potato processing, these films can be stabilized by surface active substances such as proteins, carbohydrates and other naturally occurring or process derived compounds. Defoamers control foam mainly through physical and interfacial mechanisms rather than through a chemical reaction.
- Entry into the foam film — Defoamer droplets are dispersed in the process liquid and come into contact with the foam lamellae.
- Spreading at the air–liquid interface — When the defoamer has suitable interfacial properties, it enters and spreads over the foam film. Its effectiveness depends on factors such as surface tension, interfacial tension and compatibility with the liquid phase.
- Destabilization of the film — The defoamer disrupts the arrangement of surface-active compounds that stabilize the lamella. This creates local areas of reduced film stability and promotes thinning.
- Bridging and de-wetting — In formulations containing hydrophobic particles or other active components, these materials can interact with the film through mechanisms commonly described as bridging de-wetting or related interfacial effects. This further weakens the lamella.
- Film rupture and bubble collapse — Once the film becomes sufficiently thin and unstable, it ruptures. The air bubble collapses and the entrained air is released.
The effectiveness of a defoamer depends on its dispersion, droplet size, interfacial properties, concentration, temperature, pH and compatibility with the process liquid. The composition of potato processing water including starch, proteins, dissolved solids and other surface-active materials can also significantly affect performance.
Defoamer dosage should therefore be optimized through process trials. Overdosing does not necessarily improve foam control and can increase product cost, create carry over or residue concerns or interfere with other process operations. Processors generally aim to use the lowest effective dosage that provides reliable foam control under actual plant conditions.
How Defoaming Agents Work in Potato Processing
Food-Grade Defoamers: Regulatory Requirements for Potato Processing
Food-grade status is important when defoamers are used in potato processing because some applications involve process water or other streams that may come into contact with food. However, “food-grade” is not a universal regulatory approval. The permitted composition, application, maximum use level and residue requirements depend on the specific product and the market in which it is used.
In the United States, 21 CFR Section173.340 regulates defoaming agents used in food processing. Dimethylpolysiloxane is permitted at a maximum of 10 ppm in food in its ready-to-consume state, subject to specified exceptions, including zero in milk, 110 ppm in certain dry gelatin dessert mixes and 250 ppm in salt intended for cooking, provided the resulting food meets the applicable limits. The regulation also specifically permits white mineral oil conforming to 21 CFR Section172.878 as a component of defoaming agents used in wash water for sliced potatoes at a level not exceeding 0.008% of the wash water. Other substances are permitted under the conditions and limitations specified in the regulation.
In the European Union, dimethylpolysiloxane (E 900) is an authorized food additive under Regulation (EC) No 1333/2008, but its permitted uses and maximum levels are defined by specific food categories and conditions of use. For example, the Union list includes E 900 at 10 mg/kg for oils and fats for frying; this should not be interpreted as a general 10 mg/kg limit for all potato processing applications. The regulation also distinguishes food additives from processing aids, which are outside its scope when they are used as processing aids rather than as food additives. Therefore, a defoamer used during potato washing or other processing operations must be assessed according to its actual use, composition and regulatory status.
Requirements in other major markets, including countries that follow or reference Codex standards and national food regulations across Asia, Latin America and other regions can differ in how defoamers are classified and what substances and use levels are permitted. For international potato processors, the regulatory status of the specific commercial formulation should therefore be verified rather than relying only on the term “food-grade.” Suppliers commonly provide Technical Data Sheets, Safety Data Sheets, regulatory statements, specifications and where applicable, allergen, Kosher and Halal documentation. Organic claims require separate verification against the relevant organic standard.
Under GMP and HACCP-based food safety systems, processors should control the identity, permit application, concentration and dosing of defoamers and maintain documentation demonstrating that their use complies with the applicable regulations and customer requirements. Whether a product is authorized for direct food use, permitted as a processing aid or suitable only for indirect food contact applications must be verified for the specific formulation, process and destination market. A product approved unauthorized one jurisdiction should not automatically be assumed to be approved for the same use worldwide.
Defoaming Agents in Potato Starch Processing
Potato starch plants can generate significant foam at several stages, particularly during rasping, starch pulp separation and potato juice handling. After washing, potatoes are rasped to rupture the cells and release starch granules, potato juice and pulp. The resulting slurry can become highly foam prone because potato proteins have strong surface active and foam stabilizing properties, while mechanical shear, turbulence and air incorporation promote foam formation.
Foam control is important because excessive foam can interfere with pumping, screening, starch pulp separation and the recirculation of process water. It can also contribute to unstable process conditions and equipment overflow. Studies on potato starch production have identified foam destruction as important for maintaining process water recirculation and controlling water consumption.
Potato juice, also called potato fruit juice is separated from the starch stream and may be heated for protein coagulation or further protein recovery. Because potato proteins have significant foaming properties, heating and subsequent handling can create persistent foam. Industry guidance for potato starch production identifies antifoam use around the coagulation stage, while some modern plants use mechanical defoaming systems instead of chemical antifoams.
Downstream refining, washing, concentration and dewatering can also require foam management depending on the plant design and operating conditions. Effective foam control helps maintain stable flow and reliable operation of separation equipment and process water circuits. The choice between chemical defoamers and mechanical foam control systems depends on the process, product requirements and regulatory conditions.
Defoaming Agents in French Fry and Potato Chip Processing
In French-fry lines, foam appears primarily in the washing, cutting, rinsing and starch removal flumes. Free starch liberated during cutting accumulates in recirculated water and together with proteins, stabilizes foam. Continuous or automated dosing of a suitable food grade defoamer keeps transport water clear, prevents tank overflows and maintains design line speeds through blanching and further processing.
Potato chip (crisp) production presents similar challenges at the washing and slicing stages. Starch released into the water circuit builds up rapidly, generating persistent foam that can carry into blanching or affect slice quality and frying consistency. Defoamers are commonly injected into the washer and starch recovery loops. Products effective at the moderate temperatures typical of these circuits (often 20–40 °C) and compliant with food contact rules help maintain production efficiency and product quality. Case studies from chip plants confirm measurable improvements in foam control and reduced chemical consumption when the correct product and dosing strategy are applied.
Defoamers for Potato Processing Wastewater
Potato processing wastewater can contain high levels of starch, proteins and other organic matter. When this effluent is collected in equalization tanks or subjected to pumping, mixing and aeration during biological treatment, these conditions can generate significant foam. Excessive foam can cause tank overflow, disrupt aeration and dissolved oxygen control, complicate equipment operation and create housekeeping and safety problems.
The choice of defoamer for wastewater treatment is important because the product can enter downstream biological treatment systems. A suitable formulation should not adversely affect the microorganisms responsible for wastewater treatment at the intended dosage. Compatibility with activated sludge, anaerobic digestion and other treatment processes should therefore be evaluated before use. The defoamer should be applied at the lowest effective dose to control foam without unnecessarily increasing chemical consumption or affecting effluent quality.
Silicone-based, silicone free and bio-based defoamers are available for industrial wastewater applications. The most suitable option depends on the type of foam, treatment process, water chemistry, discharge requirements and operating conditions. Effective foam control helps maintain stable wastewater treatment operations while reducing overflow risks, chemical waste and operational interruptions.
Key Factors in Selecting a Defoaming Agent for Potato Processing
Choosing the right defoamer requires matching its performance to the specific conditions of the processing plant. Key selection factors for process engineers and procurement teams include:
| Factor | Why it matters |
|---|---|
| Processing temperature | Performance changes with temperature; products must remain effective from cold wash water to warmer blanching or heating steps. |
| pH range | Influences both foam stability and chemical compatibility of the defoamer. |
| Foam type | Surface foam versus entrained air may favor different chemistries or droplet characteristics. |
| Starch concentration | Higher starch loads often demand more robust or higher activity formulations. |
| Protein content | Proteins stabilize foam; products proven in protein rich systems perform more reliably. |
| Water quality | Hardness, dissolved solids and degree of recirculation affect dispersion and longevity. |
| Food-contact status | Determines regulatory pathway, documentation needs and residual limits for the target market. |
| Processing stage | Washing, starch extraction, blanching or wastewater each present different condition. |
| Dosage efficiency | Lower effective dose reduces cost and minimizes potential downstream impact. |
| Wastewater compatibility | Important if process water enters biological treatment systems. |
| Product carryover risk | Critical for finished product quality, sensory attributes and customer specifications. |
Additional practical considerations include the supplier's technical support, availability of plant trial data, dosing method, dilution requirements, storage stability and certifications required by customers or target markets, such as Kosher or Halal certification. Organic claims should be assessed separately because requirements vary by certification scheme and market.
The most reliable selection method is an on-site trial under actual processing conditions. Laboratory testing can help screen products, but plant trials provide a better indication of performance under real temperature, pH, starch load, water quality, flow and recirculation conditions.
Cost should also be evaluated based on cost per effective foam control result, rather than purchase price alone. A higher priced defoamer may be more economical if it requires a lower dosage, lasts longer, reduces process interruptions or provides more consistent foam control.
Defoamer Dosage and Application Methods
There is no single dosage rate suitable for all potato processing operations. The required amount depends primarily on the type and concentration of the defoamer, the severity of foaming, process flow and the point of application. Manufacturers normally provide an initial dosage range, which should be verified and optimized through controlled plant trials.
Common application methods include:
- Continuous dosing — An automatic dosing pump delivers a controlled amount of defoamer into the process water line or other designated injection point.
- Intermittent dosing — Small quantities are added periodically when foam reaches a defined operating level.
- Automatic foam control — Foam sensors or probes can activate or regulate dosing according to changes in foam levels.
- Point-of-application dosing — Defoamer is introduced close to locations where foam is generated, such as washer circuits, flume returns or starch recovery systems.
Depending on the product and dosing equipment, the defoamer may be applied directly or diluted before injection to improve distribution. The optimum rate is normally established by starting at the lower end of the supplier's recommended range and increasing gradually until effective foam control is achieved.
During trials and routine production, operators should monitor foam levels, product quality, process performance and any effects on downstream operations. Excessive dosing can increase chemical consumption and may create unwanted process effects making accurate metering important.
Once the effective dosage has been established, maintaining a consistent and controlled feed is generally preferable to large corrective additions. Plants should record dosage rates, injection locations, operating conditions and trial results to support ongoing process optimization and consistent foam control.
Key Benefits of Foam Control in Potato Processing
Effective foam management can provide several operational and economic benefits across potato processing operations:
- Higher and more consistent throughput by reducing foam related interruptions and process slowdowns.
- Lower risk of tank and vessel overflow, helping prevent losses of process water, slurry or product containing streams.
- More reliable equipment operation, particularly for pumps, screens, centrifuges, level sensors and other systems affected by excessive foam.
- Greater process stability by maintaining more consistent operating conditions during water intensive processing steps.
- Reduced unplanned downtime associated with foam related interventions, cleaning or equipment adjustments.
- Improved water management by reducing the need for emergency flushing, dilution or process water replacement.
- More consistent starch separation and recovery when excessive foam interferes with screening, separation or slurry handling.
- Lower cleanup requirements where foam overflow would otherwise leave residues around tanks, equipment and production areas.
- Potential operating-cost savings when foam control is achieved with an optimized defoamer dosage and application strategy.
Overall, effective foam control can support higher plant uptime, smoother operation, more predictable production and lower costs associated with interruptions, cleanup and inefficient process water management.
Problems Caused by Poor Foam Control in Potato Processing
Inadequate foam control can create a range of operational and maintenance problems in potato processing plants:
- Tank and vessel overflows that can result in losses of process water, product containing streams and chemicals while increasing housekeeping and safety risks.
- Reduced processing capacity when excessive foam limits usable vessel volume or requires equipment to operate below its intended throughput.
- Pumping difficulties caused by air entrainment, which can reduce flow stability and under certain conditions, contribute to cavitation and equipment wear.
- Reduced separation efficiency in screens, hydro cyclones, centrifuges and other separation equipment when excessive foam disrupts normal operation.
- Interference with sensors and probes when foam accumulates on level, conductivity or other process monitoring devices.
- Unreliable level measurement because foam can be detected as part of the liquid interface, increasing the risk of inaccurate filling or process control.
- Unplanned production interruptions caused by foam related adjustments, cleanup, equipment checks or process instability.
- Additional wastewater treatment challenges when excessive foam reaches collection, aeration or biological treatment systems.
Persistent foam problems can therefore increase operating and maintenance costs while making process control less predictable and increasing the risk of quality, environmental or regulatory issues.
Environmental and Sustainability Aspects of Defoamers
Sustainability is becoming an increasingly important consideration when potato processors evaluate defoamers. Beyond foam control performance, plants may assess the product's biodegradability, raw material sources, wastewater compatibility, regulatory status and overall chemical consumption.
- Bio-based formulations — Defoamers made partly or wholly from renewable feedstocks, such as vegetable oils or fatty alcohols are increasingly available as alternatives to some petroleum derived formulations. However, bio-based content alone does not determine overall environmental performance.
- Biodegradability — Products with favorable biodegradation profiles can help reduce the persistence of chemical components in wastewater, provided they are appropriate for the specific treatment system and application.
- Silicone and mineral oil free options — These may be preferred where particular processing requirements, customer specifications, wastewater considerations or regulatory conditions limit the use of certain ingredients.
- Lower effective dosage — A defoamer that provides reliable foam control at a low application rate can reduce overall chemical consumption and the quantity entering downstream wastewater streams.
- Wastewater compatibility — The product should be assessed for potential effects on biological treatment, including activated sludge and anaerobic processes, particularly when process water is recycled or discharged to on-site treatment.
- Regulatory and customer requirements — Product selection may also need to align with regional chemical regulations, wastewater discharge requirements, customer specifications and corporate sustainability targets.
Suppliers are increasingly developing defoamers that aim to combine effective foam control with improved environmental profiles. For processors, however, sustainability should be evaluated alongside technical performance, dosage requirements, cost, regulatory compliance and the product's overall environmental profile.
Proper product selection, accurate dosing and effective process control remain important for minimizing unnecessary chemical consumption and reducing the environmental impact of foam control operations.
Defoamer vs. Antifoam: What’s the Difference?
Although the terms are frequently used interchangeably in the potato industry, a technical distinction exists:
| Feature | Defoamer | Antifoam |
|---|---|---|
| Main purpose | Break existing foam | Prevent foam formation |
| Typical use | Foam already present | Foam prone process |
| Primary action | Rapid foam collapse (knock-down) | Foam suppression (hold-down) |
| Potato processing | Applied when foam appears | Dosed proactively into circuits |
Most commercial products designed for potato processing provide both functions to varying degrees. The practical choice depends on whether the priority is immediate knockdown of established foam or longer-term prevention in continuously circulating systems. Plant trials help determine the product and dosing strategy that best matches the dominant foam behavior at each stage.

