
The Role of Enzymes in the Global Potato Industry
The Role of Enzymes in the Global Potato Industry Enzymes play an important role in potato processing, influencing colour, texture, acrylamide formation, starch conversion and the recovery of useful materials from processing waste. They help processors improve product quality, manufacture starch-based ingredients and investigate ways to convert potato residues into higher-value products.
An enzyme is a biological catalyst, usually a protein, that speeds up a specific chemical reaction without being consumed in the process. Some enzymes occur naturally in potato tubers and influence their properties during storage, cutting and processing. Others are produced commercially, often through microbial fermentation and added under controlled conditions to achieve specific results.
For potato processors, enzymes are particularly relevant to product quality, starch conversion and waste valorisation. They can help manage enzymatic browning, modify texture and reduce acrylamide formation. In starch processing, alpha-amylase, glucoamylase and pullulanase break down potato starch into products such as maltodextrins, glucose syrups and fermentable sugars. Pectinases, cellulases and amylases can also help process potato peel, pulp and other residues for the recovery of sugars, fibres and potential bio-based products.
Alpha-amylase breaks down starch into shorter carbohydrate chains during liquefaction, while glucoamylase releases glucose and pullulanase can improve conversion by breaking down certain starch branch points. The final glucose yield depends on the starch source, enzyme combination and processing conditions.
L-asparaginase converts free asparagine into aspartic acid and ammonia, reducing the availability of an important precursor of acrylamide in fried potatoes. Published studies have reported reductions of 60–85% under specific experimental conditions, although results vary with treatment and processing parameters.
Polyphenol oxidase (PPO) contributes to enzymatic browning when cut potato tissue is exposed to oxygen. Darkening during frying is a different process involving reducing sugars and amino acids through the Maillard reaction. Invertase can influence sugar levels by breaking down sucrose, but its effect on fried colour depends on the conditions.
Pectin-modifying enzymes can influence potato tissue firmness, but their effects depend on the enzyme, potato variety and processing conditions. A temperature range of 60–70 °C should not be treated as a universal activation range for texture modification.
Commercial potato peeling commonly relies on steam, abrasion or mechanical methods. Enzymatic peeling is more challenging because the protective, suberised tissues of potato skin limit enzyme access.
Pectinases, cellulases and amylases can help break down selected components of potato-processing residues. Potential applications include sugar recovery, fibre-rich ingredients and feedstocks for fermentation and other bio-based processes.
Enzymes in the Potato Industry: Processing, Quality Improvement and Waste Valorisation
What Are Enzymes?
Enzymes are biological catalysts, almost always proteins, that lower the activation energy a reaction needs. Each enzyme has an active site shaped to bind one substrate, or a narrow family of substrates. The enzyme and substrate form a temporary enzyme–substrate complex, the reaction takes place, the product is released, and the enzyme is free to act again.
This specificity is what makes enzymes so useful in food processing. An alpha-amylase cuts only alpha-1,4 bonds in starch. L-asparaginase converts only the amino acid asparagine. Neither touches the protein, fat or vitamins around it, so a processor can change one property without disturbing the rest of the product.
Enzymes are grouped by the reaction they catalyse. Most enzymes used in potato processing are hydrolases, which split bonds by adding water (amylases, glucoamylase, pullulanase, asparaginase, pectinases, cellulases). Polyphenol oxidase is an oxidoreductase, which transfers electrons and uses oxygen.
Naturally occurring enzymes versus commercially added enzymes
Native (endogenous) potato enzymes are part of the living tuber. The most important for processors are:
- Polyphenol oxidase (PPO): oxidises phenolic compounds when cells are damaged, causing enzymatic browning and blackspot bruising.
- Peroxidase (POD): also contributes to browning and off-flavours; often used as an indicator of blanching adequacy because it is relatively heat-stable.
- Vacuolar invertase: splits sucrose into glucose and fructose, especially in cold storage. This "cold-induced sweetening" raises reducing sugars, which darken fries and chips and increase acrylamide.
- Pectin methylesterase (PME): activated when tissue is held at about 50–70 °C (most strongly around 60–70 °C); it modifies cell-wall pectin and firms texture during low-temperature blanching.
- Starch-degrading enzymes and starch phosphorylase: involved in the starch–sugar balance during storage and sprouting.
- Lipoxygenase and patatin (a lipid acyl hydrolase): linked to flavour changes and off-notes in stored or processed products.
Commercial (exogenous) enzymes are produced by controlled fermentation of microorganisms such as Bacillus, Aspergillus and Trichoderma. They are standardised for activity, purified and sold as liquids or granulates. Examples include thermostable alpha-amylases for starch liquefaction and L-asparaginase products such as Acrylaway® (from Aspergillus oryzae, Novonesis, formerly Novozymes) and PreventASe® (from Aspergillus niger, dsm-firmenich).
In simple terms, potato processors usually try to control native enzymes and use commercial ones.
Factors affecting enzyme activity
- Temperature: activity rises with temperature up to an optimum, then falls as the protein unfolds (denatures). This is why blanching inactivates PPO, and why starch liquefaction needs heat-stable bacterial amylases.
- pH: each enzyme has a working pH range. Potato PPO is most active near neutral pH (about 6–7) and slows sharply under acidic conditions, which is why citric and ascorbic acid dips limit browning.
- Time: longer contact means more conversion, but process lines have fixed residence times. Enzyme dose and time are often traded against each other.
- Substrate availability: an enzyme only works on what it can reach. Starch must be gelatinised before amylases act quickly. Asparaginase works on the surface of a fry strip far better than in its core.
- Water activity, inhibitors and cofactors: enzymes need free water. PPO needs copper and oxygen. Sulphites, ascorbic acid, calcium salts and chelators can slow or block specific enzymes.
Major Enzymes Used in the Potato Industry
Six enzyme groups dominate potato processing: three starch-converting enzymes, one food-safety enzyme, one native enzyme that must be controlled, and the cell-wall-degrading enzymes.
Amylases: Alpha-amylases (EC 3.2.1.1) randomly cut the internal alpha-1,4 glycosidic bonds of amylose and amylopectin. They rapidly reduce the viscosity of gelatinised starch and produce dextrins and maltodextrins. Thermostable bacterial alpha-amylases, mostly from Bacillus licheniformis and related species, are used for starch liquefaction at roughly 90–110 °C. Beta-amylase and fungal or maltogenic amylases produce maltose-rich syrups.
Alpha-amylase alone cannot break the alpha-1,6 branch points of amylopectin. Prolonged action leaves "alpha-limit dextrins" that need other enzymes to finish the job.
Glucoamylase: Glucoamylase (amyloglucosidase, EC 3.2.1.3), usually from Aspergillus niger, removes single glucose units from the non-reducing ends of starch chains. It hydrolyses alpha-1,4 bonds quickly and alpha-1,6 bonds slowly. It is the main saccharification enzyme for glucose (dextrose) syrup and for producing fermentable sugars for ethanol and other fermentations. It typically works at about pH 4–4.5 and 55–65 °C.
Pullulanase: Pullulanase (EC 3.2.1.41) is a debranching enzyme that specifically cuts alpha-1,6 bonds. Added during saccharification together with glucoamylase, it removes branch points faster, raises the final glucose yield, reduces unwanted by-products and allows saccharification at higher dry solids. Debranching with pullulanase is also used to make high-amylose fractions and resistant starch.
L-asparaginase: L-asparaginase (EC 3.5.1.1) converts free asparagine into aspartic acid and ammonia. Asparagine reacts with reducing sugars in the Maillard reaction above about 120 °C to form acrylamide, a probable human carcinogen. Removing asparagine before frying therefore removes a key acrylamide precursor without significantly changing colour, flavour or texture. Food-grade asparaginases are produced from Aspergillus oryzae and Aspergillus niger.
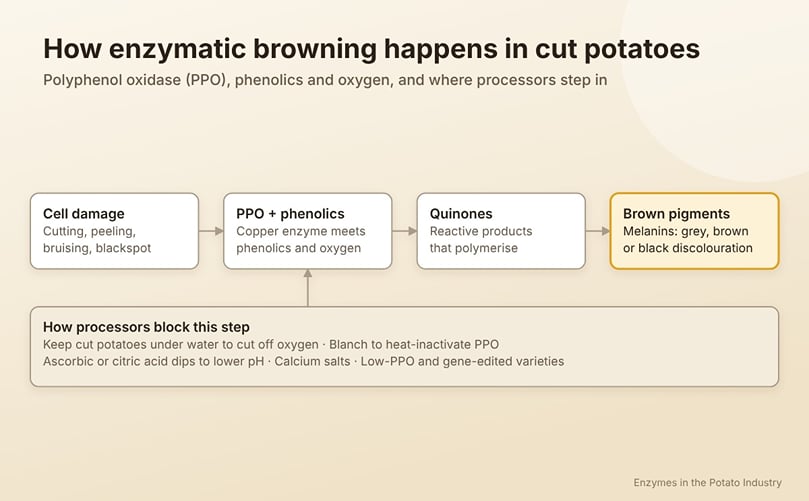
Polyphenol oxidase (PPO): PPO (catechol oxidase, EC 1.10.3.1) is a copper-containing enzyme native to the potato. When cells are cut, bruised or peeled, PPO meets phenolic substrates such as tyrosine and chlorogenic acid and, in the presence of oxygen, turns them into quinones. These polymerise into brown, grey or black melanin pigments. Studies of potato PPO report maximum activity near pH 6.5–7 and 30–40 °C, with complete heat inactivation at about 80 °C for 30 minutes. Processors almost never add PPO; they inhibit it.
needs: the active enzyme, oxygen or a suitable pH.
How Enzymatic Browning Happens in Potatoes
Pectinases and cellulases: Pectinases (polygalacturonase, pectin lyase, pectin methylesterase) and cellulases (endo- and exo-glucanases, beta-glucosidase), mostly from Aspergillus and Trichoderma, break down the plant cell wall. In the potato industry they are used or studied for releasing starch from tissue, reducing viscosity of pulp, enzymatic peeling, fibre and pectin extraction from potato pulp, and saccharification of peel and pulp for biofuels.
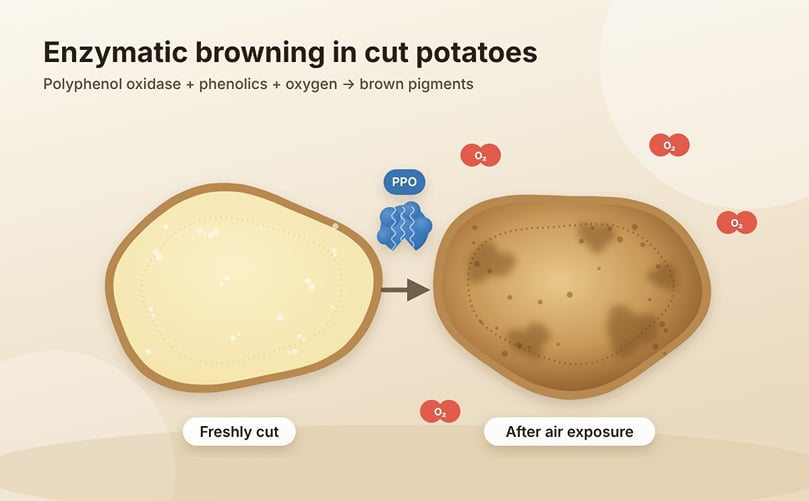
Enzymatic Browning in Cut Potatoes
Applications of Enzymes in Potato Processing
Potato Starch Production and Modification
Potato starch is one of the most valuable products of the potato industry. It typically contains about 20% amylose and 80% amylopectin, has large granules, a relatively low gelatinisation temperature, high paste clarity and naturally bound phosphate groups. These properties make it an excellent raw material for both enzymatic hydrolysis and enzymatic modification.
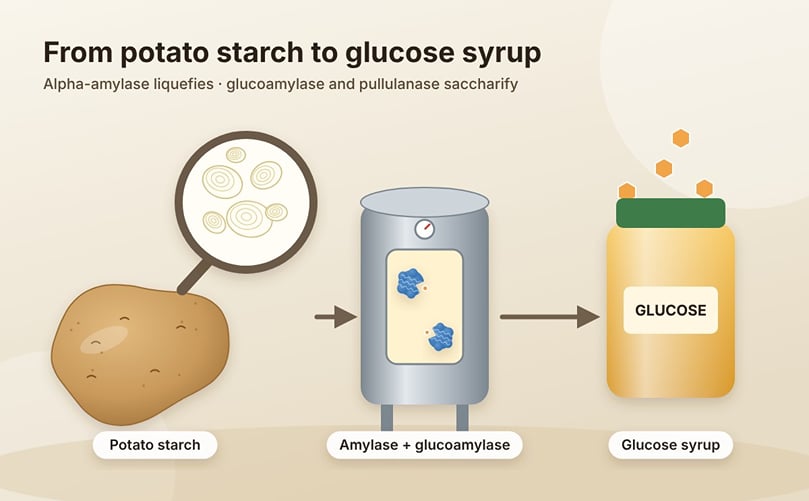
From Potato Starch to Glucose Syrup
Starch hydrolysis and conversion: Industrial conversion of potato starch into sugars follows a two-stage enzymatic process:
- Gelatinisation: a starch slurry (often 30–35% dry solids) is heated so the granules swell and become accessible to enzymes.
- Liquefaction: a thermostable alpha-amylase, often in a jet cooker at around 105–110 °C followed by holding at 90–95 °C, breaks starch into maltodextrins. The target is usually a dextrose equivalent (DE) of about 10–15.
- Saccharification: the liquefied starch is cooled to about 55–62 °C and adjusted to pH 4–4.5. Glucoamylase, often combined with pullulanase, converts dextrins into glucose over 24–72 hours, reaching glucose contents above 95%.
- Refining: the syrup is filtered, decolourised, ion-exchanged and concentrated into glucose syrup or crystalline dextrose.
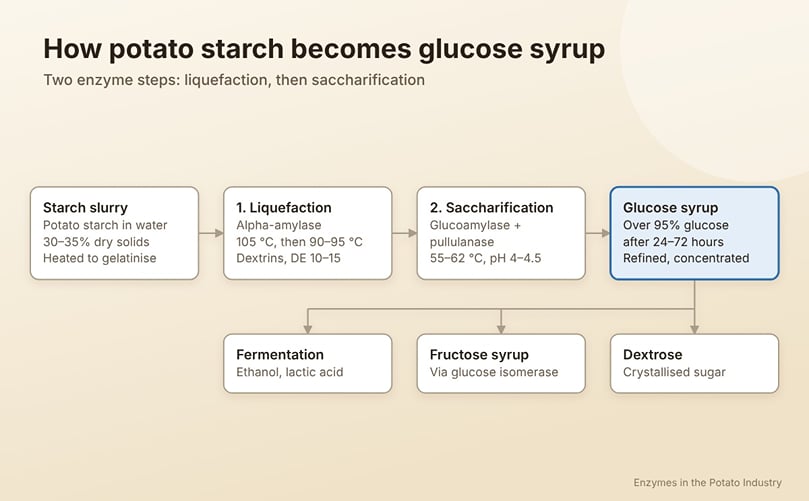
Enzymatic Conversion of Potato Starch to Glucose
Liquefaction thins the starch; saccharification finishes the job. The resulting glucose becomes dextrose, fructose syrup or a fermentation feedstock.
By stopping at different points or swapping enzymes, producers obtain a family of products: maltodextrins (DE below 20), glucose syrups, maltose syrups (with beta-amylase or maltogenic amylase) and, with glucose isomerase, fructose syrups.
Glucose production and fermentation feedstocks: Glucose from potato starch, and from cull potatoes or processing residues, is a clean fermentation feedstock. Yeast converts it to bioethanol, lactic acid bacteria convert it to lactic acid (the building block of PLA bioplastic), and other microbes produce citric acid, succinic acid, amino acids and enzymes. In simultaneous saccharification and fermentation (SSF), glucoamylase works inside the fermenter while yeast consumes the glucose as it forms. This lowers sugar inhibition, energy use and equipment needs.
Enzymatic starch modification and functional properties: Enzymes can also modify potato starch without turning it into sugar. Because no chemical reagents are used, many enzyme-modified starches can be labelled as "starch" rather than "modified starch" with an E-number, supporting clean-label claims.
- Amylomaltase (4-alpha-glucanotransferase) rearranges glucan chains. Research using Thermus thermophilus amylomaltase showed that treated potato starch forms thermoreversible gels at 3% or more, similar to gelatin. Avebe's Etenia™ is a commercial enzymatically treated clean-label potato starch used for gelatin replacement and creaminess.
- Branching enzymes add alpha-1,6 branches, producing highly branched, slowly digestible or low-viscosity dextrins for sports drinks and clinical nutrition.
- Debranching with pullulanase or isoamylase, followed by controlled retrogradation, produces resistant starch (RS3) with dietary-fibre properties.
- Partial hydrolysis with amylases creates low-DE maltodextrins for fat replacement, porous starch granules for encapsulation, and starches with lower paste viscosity.
- Cyclodextrin glycosyltransferase (CGTase) converts starch into cyclodextrins used to encapsulate flavours and active compounds.
Enzyme Activity and Quality Control in French Fries and Potato Chips
Acrylamide reduction using L-asparaginase: Acrylamide forms when free asparagine reacts with reducing sugars (glucose and fructose) during frying, baking or roasting above about 120 °C. Fried potato products are among the main dietary sources. In the EU, Commission Regulation (EU) 2017/2158 requires food business operators to apply mitigation measures and sets benchmark levels: 500 µg/kg for ready-to-eat French fries and 750 µg/kg for potato crisps.
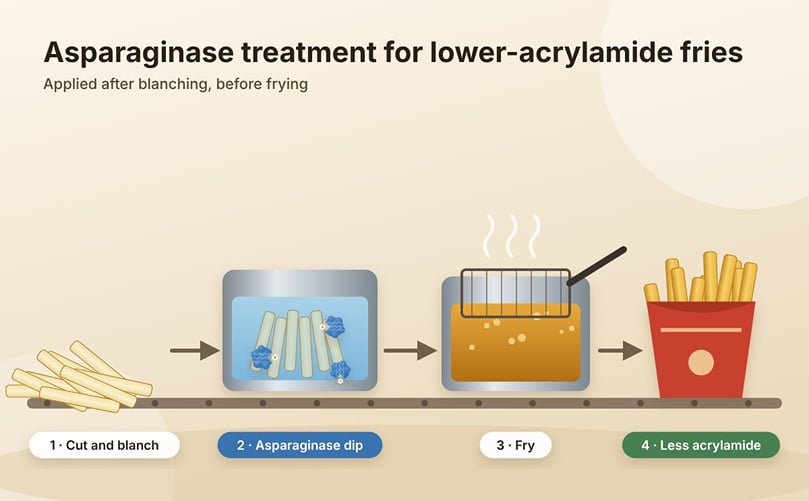
Asparaginase Treatment for Lower-Acrylamide French Fries
L-asparaginase removes the asparagine before heating. In a typical French fry line, the enzyme is applied as a dip or spray after blanching, when the cut strips are warm and the cell structure is more open. Results from published work:
Acrylamide needs both asparagine and reducing sugars. Asparaginase removes the first; storage, variety choice and blanching control the second.
- A study by Hendriksen et al. (2009) found that treating potato pieces with asparaginase after blanching cut acrylamide by 60–85% in French fries and by up to 60% in sliced potato chips. In dough-based products, reductions were 34–92%.
- Pedreschi and colleagues found that soaking unblanched strips in asparaginase reduced acrylamide by 30%, while the same treatment after blanching gave a 60% reduction.
- A 2025 study combining asparaginase with air or microwave frying reported fry acrylamide below the EU 500 µg/kg benchmark.
The key lesson is that contact matters. Whole-cut products such as fries and sliced chips are harder to treat than dough-based products, because the enzyme mainly reaches the surface. Fabricated chips, snack pellets and potato dough products made from flakes or granules give the best results, since the enzyme is mixed throughout the dough.
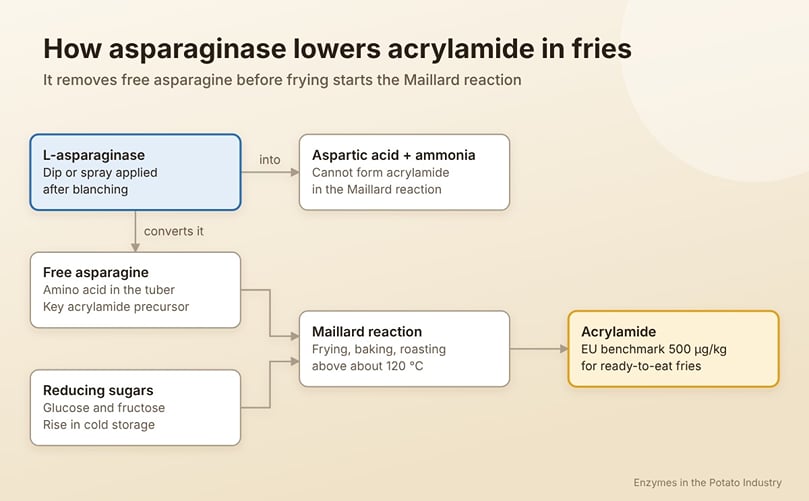
How Asparaginase Reduces Acrylamide in Fries
Enzymatic browning and colour management:
Colour in fries and chips is influenced by two separate processes:
- Enzymatic browning (PPO) happens in raw, cut or bruised potato before cooking. Cut strips that sit exposed to air turn grey or brown. Processors manage it by keeping cut potatoes under water, blanching quickly (which inactivates PPO), and using anti-browning agents such as ascorbic acid, citric acid, calcium salts and, where permitted, sulphites. Low-PPO and non-browning potato varieties also help.
- Non-enzymatic (Maillard) browning happens during frying and depends on reducing sugars and asparagine. Here, native invertase is the main enzyme of concern, because it raises reducing sugars during cold storage. Storing fry and chip potatoes at about 7–10 °C (commonly 8–10 °C) rather than 2–4 °C, reconditioning, selecting low-sugar varieties and leaching sugars during blanching keep fry colour light and even.
After-cooking darkening, a grey-blue discolouration of cooked potato, is non-enzymatic. It is caused by an iron–chlorogenic acid complex and is controlled with sodium acid pyrophosphate (SAPP).
Effects of enzyme activity on processing quality: Native enzymes also shape texture. Low-temperature blanching or "pre-heating" at about 60–70 °C activates pectin methylesterase. PME removes methyl groups from pectin, allowing calcium cross-links that firm the cell wall. The result is fries that hold their shape, break less during processing and have a better crisp-outside, fluffy-inside structure. Uncontrolled enzyme activity, by contrast, can cause soft spots, sugar ends, colour defects and off-flavours.
Enzyme Applications in Potato Flake and Purée Processing
Texture and consistency: Dehydrated mashed potato products (flakes and granules) depend on keeping potato cells intact. If too many cells rupture, free gelatinised starch is released and the reconstituted product becomes sticky and gluey. The classic precook–cool step (a mild precook, commonly cited as about 65–80 °C for 15–20 minutes, followed by cooling in cold water) uses two effects. Native PME firms the cell walls, and the cooling causes amylose to retrograde so it is less likely to leach out later. This gives a mealy, fluffy texture after rehydration.
Starch breakdown and viscosity: Free starch controls the viscosity of purées, baby food and soups. Small additions of alpha-amylase can lower viscosity in a controlled way. This is useful for pumpable potato purées, infant foods, potato-based beverages and drinkable soups. Too much amylase, however, produces a thin, sweet product, so the enzyme dose and the heat inactivation step must be tightly controlled.
Product quality and stability: Residual native enzymes in dehydrated products can cause quality loss in storage. Lipoxygenase and lipid-acyl hydrolases contribute to rancid, cardboard-like off-flavours. PPO and peroxidase can cause discolouration. Adequate blanching, antioxidant addition and low moisture help prevent these changes. For flakes destined for fabricated snacks, asparaginase can be added during dough mixing to control acrylamide.
Potato Peeling and Tissue Processing
Potential uses of pectinases and cellulases: In theory, pectinases and cellulases can loosen the skin by dissolving the cell-wall layers that bind it to the flesh. They can also macerate tissue to release starch, produce single-cell potato purées or soften tissue for infusion processes.
Enzymatic versus conventional processing methods: The potato industry overwhelmingly uses steam peeling, abrasion peeling and, less often today, lye (caustic) peeling. Steam peelers are fast, handle high throughput and work with all tuber shapes. Enzymatic peeling is gentler, uses less energy and avoids caustic chemicals, but it is much slower.
Technical limitations and commercial adoption: Potato skin is the main problem. It is a periderm made of suberised cells, which are waxy and highly resistant to enzymes. In a VTT study of enzymatic vegetable peeling, commercial cellulase and pectinase treatments greatly helped peel carrots and onions, but hydrolysis of potato peel was very limited because of its high cutin and suberin content. As a result, enzymatic peeling of potatoes remains a research topic with no meaningful commercial adoption. Enzymes are more useful in downstream tissue processing, such as pulp treatment and starch release, than in peeling itself.
Potato Waste Valorisation
Potato processing creates large side streams: peel, trimmings, cull and off-grade tubers, starch-rich process water, potato fruit juice and potato pulp from starch factories. Depending on the peeling method, a large share of tuber mass can end up as peel. Enzymes help turn these streams into products.
The same enzyme toolbox serves every side stream; the products depend on which fraction is recovered first.
Starch and component recovery: Starch-rich wastewater and fines can be recovered and either sold as feed or industrial starch or hydrolysed directly. Potato pulp, the fibrous residue left after starch extraction, is rich in pectin, especially galactan-rich rhamnogalacturonan I (RG-I), plus cellulose and residual starch.
- Researchers at the University of Copenhagen developed a large-scale enzymatic process for extracting undegraded RG-I from potato pulp. It uses an alpha-amylase to remove starch, then a purified polygalacturonase to solubilise RG-I.
- A Technical University of Denmark study found that a minimal treatment with pectin lyase and polygalacturonase at pH 6.0 and 60 °C released 75% of the pulp dry matter within one minute. The released fibres showed prebiotic (bifidogenic) potential.
Conversion of potato residues into fermentable sugars: Peel and pulp contain starch, cellulose and hemicellulose, but very little free sugar. A pre-treatment (heat, steam, mild acid or alkali) followed by enzymatic hydrolysis is therefore needed. Amylases and glucoamylase release glucose from starch. Cellulases, hemicellulases and pectinases release additional sugars from the cell walls. Enzyme cocktails from Aspergillus niger and Trichoderma reesei are commonly studied. Enzymatic hydrolysis is gentler and produces fewer fermentation inhibitors than acid hydrolysis, although enzymes add cost.
Potential production of bio-based products and other value-added materials
- Bioethanol and biogas: reviews describe peel as a promising low-cost feedstock for ethanol and biogas production.
- Lactic acid: research at the University of Idaho studied enzymatic hydrolysis of potato peel waste followed by fermentation to lactic acid, a precursor for PLA bioplastics.
- Bioplastics and films: peel starch and fibres can be cast into biodegradable films, and peel hydrolysates can feed bacteria that make polyhydroxyalkanoates (PHA).
- Dietary fibres, prebiotics and pectin: from enzymatic pulp processing, as described above.
- Bioactive compounds: enzyme-assisted extraction can release phenolic compounds such as chlorogenic acid from peel for use as natural antioxidants.
- Microbial enzymes: potato waste is also used as a cheap growth medium for producing amylases, cellulases and other enzymes, closing the loop.
Benefits of Enzyme Technology
Improved process control and product consistency: Enzymes act on one target and can be dosed in standardised activity units. This lets processors steer a single property, such as viscosity, sugar profile or asparagine content, while leaving everything else unchanged. Enzymes can also be switched off at a defined point by heat, which gives precise end-points in starch conversion and purée production. The result is more uniform products from batch to batch, even when raw potato quality varies.
Potential improvements in processing efficiency
- Enzymatic starch conversion runs at moderate temperatures and near-neutral to mildly acidic pH, so it uses less energy and fewer chemicals than acid hydrolysis. It also gives purer syrups with fewer colour and off-flavour by-products.
- Pullulanase and improved glucoamylases increase glucose yield and allow processing at higher dry solids, which saves evaporation energy.
- Enzymes in liquefaction lower viscosity quickly, making slurries easier to pump and process.
- Simultaneous saccharification and fermentation shortens the route from potato starch or waste to ethanol and other products.
Reduction of selected unwanted compounds: L-asparaginase reduces acrylamide by removing its precursor rather than changing the cooking process. This means processors can keep the golden colour, flavour and crispness consumers expect. It is one of the few acrylamide mitigation tools that does not depend on lowering frying temperature or shortening frying time.
Opportunities for resource recovery and waste reduction: Enzymes turn low-value peel, pulp and process water into fermentable sugars, dietary fibres, pectin, prebiotics and bio-based chemicals. This supports circular-economy goals, reduces disposal costs and landfill, and creates extra revenue streams from the same tonne of potatoes.
Clean-label and sustainability advantages: Enzymes are generally used as processing aids and are inactivated before the final product, so they usually do not need to be declared as ingredients in many markets. Enzyme-modified starches can replace chemically modified starches and animal-derived gelatin. Enzymes are biodegradable and are made from renewable fermentation inputs.
Key Challenges in Industrial Enzyme Applications in the Potato Industry
Enzyme costs and dosage requirements: Industrial enzymes are a recurring cost per tonne of product. For high-volume, low-margin products such as French fries, even a small added cost matters. Dosage must be optimised for each line, because too little enzyme gives weak results and too much wastes money. In continuous asparaginase baths, enzyme activity declines over time and must be topped up, so plants need monitoring routines. For waste valorisation, the cost of cellulase and pectinase cocktails is often the deciding factor in whether biofuel or chemical production is economic.
Temperature and pH sensitivity: Enzymes work only within certain temperature and pH windows. This creates conflicts with existing process steps:
- Asparaginase needs a holding step at moderate temperature (often around 40–60 °C), which may not fit a line designed for fast blanching and drying.
- Glucoamylase requires acidic conditions, so pH must be adjusted after liquefaction.
- Enzymes are inactivated by excessive heat, so processors must design for both an active window and a controlled inactivation step.
Reaction time and process integration: Enzymes need time, while modern potato lines are built for speed and continuous flow. French fry lines can process many tonnes per hour, and adding a 5–20 minute enzyme step requires space, tanks and residence-time control. Whole-cut products also limit enzyme penetration. Studies show that blanching before enzyme treatment greatly improves results, so the enzyme step must be placed carefully in the process sequence.
Raw material variability: Potatoes vary widely by variety, growing season, soil, fertilisation, storage temperature and storage time. Free asparagine, reducing sugars, dry matter, phenolic content and PPO activity all change. An enzyme dose that works in autumn may be inadequate in spring after months of storage. Processors therefore combine enzymes with good agronomy, variety selection and storage management rather than relying on enzymes alone.
Regulatory and food safety requirements: Food enzymes must be safety-assessed before use, and the rules differ by market:
- International: the Joint FAO/WHO Expert Committee on Food Additives (JECFA) evaluated asparaginase from Aspergillus oryzae in 2007 and from Aspergillus niger in 2008, assigning both an ADI of "not specified", the most favourable safety category.
- United States: food enzymes are typically used under the GRAS (Generally Recognised As Safe) framework. FDA had no objection to a GRAS notice for A. niger asparaginase.
- European Union: food enzymes fall under Regulation (EC) No 1332/2008, with EFSA safety evaluations feeding into a single Union list of authorised food enzymes. Until that list is in force, national rules continue to apply in some member states.
- Australia and New Zealand: enzymes are approved as processing aids under the Food Standards Code.
- Canada: enzymes must be listed in Health Canada's permitted enzyme lists.
Other issues include labelling (processing aid versus ingredient), allergen and source-organism declarations, the use of genetically modified production strains, and halal, kosher and vegetarian certification. Exporters must check each destination market. Enzyme dust can also be a respiratory sensitiser for workers, so liquid or granulated forms and good handling practices are needed.
Emerging Trends and Future Opportunities
Engineered enzymes and improved formulations: Protein engineering is producing enzymes that are more robust and better matched to potato lines. Examples include thermostable asparaginase variants designed to stay active longer in hot, continuous dip baths, and thermostable pullulanases that can work during liquefaction rather than only in saccharification. Improved formulations, such as liquid concentrates with stabilisers and enzyme blends tuned to specific substrates, make dosing easier and extend shelf life.
Precision control of enzyme activity: The industry is moving from fixed recipes to data-driven control. Inline sensors (near-infrared spectroscopy, colour vision systems and rapid sugar or asparagine tests) can measure raw material quality as it enters the plant. Process software can then adjust enzyme dose, temperature and holding time in real time. Precision is also being applied to native enzymes in the tuber itself:
- Simplot's Innate® potatoes use RNA interference to lower expression of genes for asparagine synthetase (Asn1), polyphenol oxidase (Ppo5) and other targets, reducing acrylamide potential and blackspot bruising. Later lines also silence vacuolar invertase.
- Researchers in Argentina used CRISPR/Cas9 to edit the StPPO2 gene in the Desiree variety. Lines with all four alleles edited showed up to 69% lower tuber PPO activity and 73% less enzymatic browning.
Regulatory acceptance of genetically modified and gene-edited potatoes varies widely between countries, which will shape how quickly these approaches spread.
Enzyme-assisted sustainable starch processing: Starch producers are exploring raw-starch-hydrolysing enzymes that work below gelatinisation temperature, lowering cooking energy. Enzymatic routes are replacing chemical modification in clean-label texturisers, resistant starches and slowly digestible carbohydrates. Enzymes also support water recycling and the recovery of potato protein and fibre alongside starch, moving starch factories toward full-tuber biorefineries.
Advanced potato waste conversion: Future biorefineries are likely to combine several enzyme steps in sequence: recovering starch and pectic fibres first, then hydrolysing the remaining cellulose and hemicellulose for fermentation. Target products include bioethanol, biogas, lactic acid for PLA, PHA bioplastics, prebiotic oligosaccharides and natural antioxidants. On-site enzyme production, using potato waste itself as the growth medium, could reduce enzyme costs significantly.
Research opportunities for industrial-scale adoption
- Improving enzyme penetration in whole-cut fries and chips, for example by combining enzymes with vacuum impregnation, pulsed electric fields or high-pressure processing.
- Developing enzymes that work at the exact temperatures and pH of existing blanching and fluming steps.
- Immobilised and reusable enzymes to lower cost per tonne.
- Techno-economic and life-cycle studies that prove the business case for waste valorisation at plant scale.
- Better understanding of how variety, climate and storage affect enzyme-relevant compounds, so treatments can be predicted rather than adjusted after the fact.