

Forklift Dumper
PFI Forklift Dumper unloads bulk product containers quickly, improving the production and efficiency of your food processing line without compromising safety or traffic.

SB 651 Receiving hopper of 12-14 m³
The SB 651 is a high-performance receiving hopper with a bunker capacity of 12-14 m³ and a 2 metre wide product-friendly bunker floor. Various units can be positioned downstream of the bunker.

Self-cleaning and disinfecting screw conveyor
The automatically controlled process leads to complete control of water and chemical consumption. The automatically controlled process leads to complete control of water and chemical consumption.

Special Processing and Packaging Conveyors
CMP manufactures a wide range of custom conveyor systems to meet specific client processing demands.

Roller Conveyor
The Kanchan Roller Conveyor for Cartons is an ideal solution for efficiently transferring finished goods cartons from the packaging area to the storage area.
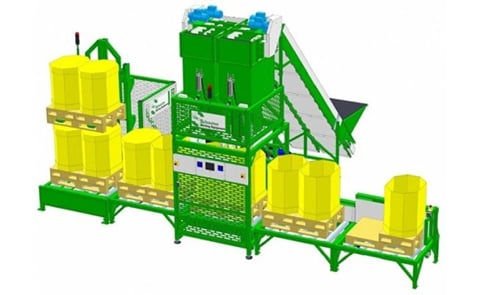
Octabin Filler
Complete system to automatically weigh, fill and stack octabins (boxes of 200 kg). Capacity of 30 pallets per hour, 2 minutes per pallet.
Sponsored Content
Sponsored Content
Sponsored Content

Mini VF Electromagnetic Vibratory Motion Conveyor
The PPM Technologies Mini VF is a small yet powerful electromagnetic vibratory motion conveyor that boasts a variety of versatile mounting options, adjustable feed rates, an open and sanitary design, low maintenance costs, and a long and dependable life cycle.

Conveyors for Frozen Food
Designed to meet the stringent hygiene and safety requirements of the frozen food industry, these conveyors ensure seamless, contamination-free product movement throughout the processing line.

Tote Dumpers
PPM Technologies crate and tote handling systems make filling and unloading efficient and easy. PPM’s dump and fill units work together or separately as economical, effective solutions to handling bulk storage prior to final processing.

Feeding-Hopper
The Feeding-Hopper with Discharge System from Kanchan Metals is designed to store and dispense bulk materials efficiently and uniformly.

BL conveyor
The PPM Technologies BL conveyor was designed for high-volume or heavy-head-load applications, using a mechanical crankshaft and belt/pulley system powered by a variable-frequency motor.

Inclined or Vertical Elevators
Tecno Alimentaria Valenciana (TAV) have two models: standard and with external chassis. The external chassis allows the interior cleaning, it is accessible to have control points, and in this way to control that there are no product remains inside.
Sponsored Content

SB 151 Receiving hopper of 5–6 m³
The SB 151 is the smallest receiving hopper (5–6 m3 bunker capacity) from the Dewulf product range. However, the machine is equipped with the necessary features. This receiving hopper is the right choice for smaller growers.

Purlift
Purlift positive drive vertical lift conveyor fits in tight spaces where you need to elevate your food processing line. Its positive drive system and self-tracking belt keep your product and operation moving.

Vibratory Sizer and Graders
The CMP line of vibratory shakers have been designed to sort or size food products of all shapes and sizes.

Horizontal Belt Conveyor
PFI Horizontal Belt Conveyors are common conveying solutions to move product throughout your food processing plant.

Retractor
PFI Retractor retracting belt conveyor adds flexibility to the fixed space of your food processing plant. It performs several applications in one machine – from loading and depositing to transferring, rejecting, and positioning.

Scale Feed
FoodeQ designs and builds professional shakers exactly according to their customers’ requirements and wishes for a wide range of products and purposes. They build scale feeding vibratory conveyors in all shapes and sizes for product supply for multi-head weigh systems.