

H-Flow Conveyor
FoodeQ designs and builds H-Flow conveyors exactly according to their customers’ requirements and wishes, for the gentle horizontal handling and conveying of delicate food products.

CentreQ
FoodeQ introduces CentreQ®, a pioneering monitoring system for vibrators driven by unbalance motors. CentreQ® is a software tool that measures and adjusts the behavior of the vibrator.

Even Flow Bins
CMP Manufactures several styles of even flow bins to provide surge capacity in raw receiving applications as well as other process and packaging areas.

Dewatering Shaker
FoodeQ designs and builds professional shakers exactly according to our customers’ requirements and wishes for a wide range of products and purposes.
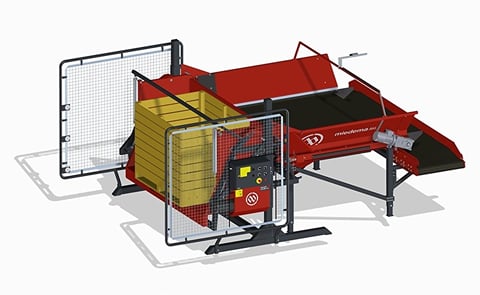
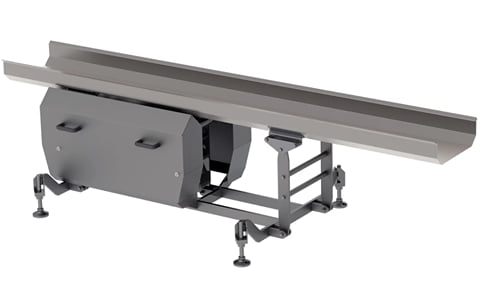
Purmotion
PFI Purmotion horizontal motion conveyor smoothly conveys a variety of products throughout your food processing line.
Sponsored Content
Sponsored Content
Sponsored Content

Conveyor
PFI Conveyor fit tight turns and transfers. Seamlessly move your product around turns, corners, and other equipment then gently transfer it to the next step.

A self-cleaning and disinfecting transport system
A self-cleaning and disinfecting transport system for frozen food that can transport 1 ton/h to 60 ton/h products over longer and steep sections.

Sanitary Conveyor–Endless Plastic Belt–Flat Style
CMP routinely works with leading solid plastic belt manufacturers including Intralox Thermodrive and Volta to deliver best in class sanitary conveyor solutions.

Bucket-Elevator
PFI Bucket Elevator conveyor elevates your product to the next step in your food processing line in a tight footprint.


Ultra Conveyor
The PPM Technologies Ultra conveyor was designed to accommodate a wide range of products and applications, including heavy, hard-to-move products such as meat, poultry, fruits or vegetables.
Sponsored Content
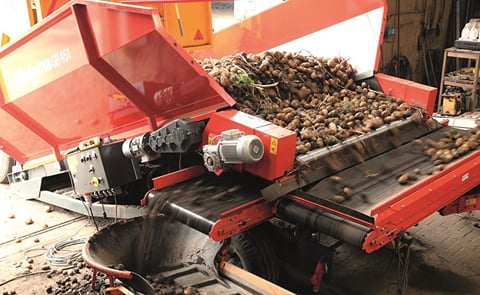
SB 451 Receiving hopper of 10-12 m³
The SB 451 is a small receiving hopper with large capacities and has a bunker capacity of 10-12 m³. This product-friendly receiving hopper can be equipped with a combination of various options both in the field of cleaning and sorting.

Dewatering Vibratory Conveyors
Vibratory conveyor to separate product from a water flow. Water will flow back to the pump system and the product will be transported straight forward.

Accumulation Trays
Optimize product flow regulations and homogenize the flow rate, using accumulation hoppers as required.
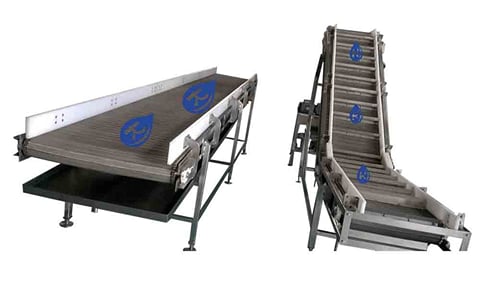
Conveyors for Snacks
Kanchan Metals offers a range of conveyors specifically designed for the snacks industry. These conveyors are engineered to handle various types of snacks.

Vibratory Length Graders
FoodeQ has experience in grading/sorting a wide range of products, including french fries.

Eleveyor
PFI Eleveyor elevate production to new heights.
Seamlessly elevate your product to the next step in your process with minimal product waste on a clean, dependable incline belt conveyor.
Seamlessly elevate your product to the next step in your process with minimal product waste on a clean, dependable incline belt conveyor.